For a popcorn factory, a production line rated at 100 kg/h does not necessarily produce 800 kg of finished popcorn during an eight-hour shift. Cleaning, product changeovers, equipment stoppages, seasoning, and packaging can all reduce the amount of saleable product leaving the factory.
The difference between rated capacity and actual output is essential when evaluating popcorn production efficiency. Manufacturers need to understand not only how much popcorn a machine is designed to produce, but also how much finished product the entire production line can deliver under normal operating conditions.
Rated capacity is the output specified for a machine or production line under defined operating conditions. Actual output is the quantity of product the factory really produces during a measured period. By comparing these figures, popcorn manufacturers can identify production losses, evaluate equipment performance, and make better decisions about automation and capacity expansion.
For factories planning new equipment, XFD provides industrial popcorn production equipment designed for different manufacturing requirements, including electromagnetic popping systems and hot-air production lines.
What Is the Difference Between Rated Capacity and Actual Output?
Rated capacity describes the production rate associated with a particular machine configuration. Actual output measures what the equipment and its operators achieve in real production.
For example, a popcorn production line rated at 80 kg/h has a theoretical output of 640 kg over eight hours of continuous production at its rated rate. However, the factory may produce only 520 kg of finished popcorn during the same scheduled shift because of cleaning, flavor changes, ingredient replenishment, and temporary stoppages.
In this example, the rated output is 640 kg, while the actual output is 520 kg. The difference is 120 kg.
It is also important to confirm what the manufacturer's capacity specification measures. Depending on the equipment and quotation, the figure may refer to popped popcorn, coated popcorn, or another production stage. A factory should not compare different capacity figures until the measurement basis has been confirmed.
When evaluating a new large-scale popcorn production and coating line, buyers should ask for the rated output, the product and recipe used for testing, and the expected finished-product output under their own operating conditions.
How Can Popcorn Factories Calculate Production Efficiency?
The simplest way to evaluate production efficiency is to compare actual output with rated output over the same period. Both figures must use the same product stage, unit of measurement, and time basis.
Production efficiency formula:
Production Efficiency (%) = Actual Output ÷ Rated Output × 100%
Suppose a popcorn production line has a rated capacity of 80 kg/h and operates during an eight-hour scheduled shift.
Step one: Calculate the rated output.
80 kg/h × 8 hours = 640 kg
Step two: Record the actual output.
Assume the factory produces 520 kg of finished popcorn during the shift.
Step three: Calculate production efficiency.
520 kg ÷ 640 kg × 100% = 81.25%
The production efficiency for this example is 81.25% when measured against the rated output over the scheduled shift.
This is a simplified output-based indicator, not a universal measure of overall equipment effectiveness (OEE). It does not independently measure availability, operating speed, or product quality. Factories that want a more detailed performance analysis should track these factors separately.
What Does a Realistic Production Calculation Look Like?
A useful production report should show how the theoretical production target compares with the actual quantity produced and the time lost during the shift.
| Production Metric | Example |
|---|---|
| Rated production capacity | 80 kg/h |
| Scheduled production time | 8 hours |
| Theoretical output | 640 kg |
| Actual finished output | 520 kg |
| Output-based production efficiency | 81.25% |
| Output difference | 120 kg |
The 120 kg difference does not automatically mean that the machine is underperforming. The factory needs to investigate whether the gap comes from planned cleaning, unplanned downtime, product changeovers, popping losses, or a bottleneck further down the line.
For example, the popping machine may be capable of producing popcorn faster than the coating or cooling equipment can process it. In this case, increasing the popper's rated capacity alone will not necessarily improve finished output.
This is why manufacturers should evaluate the complete process when comparing industrial popcorn equipment, rather than relying on one machine's maximum rated output.
Which Factors Reduce Actual Popcorn Production Output?
Several operating conditions can create a gap between rated capacity and actual output. Recording these factors helps factory managers identify where production time and finished product are being lost.
Equipment downtime: Unexpected stoppages, electrical issues, maintenance, and equipment adjustments interrupt production. Even short interruptions can accumulate over a full shift.
Popping cycle time: The time required to load kernels, heat the kettle, complete popping, discharge the product, and prepare for the next batch affects hourly output. Different heating technologies and machine configurations may have different cycle times.
Ingredient replenishment: Operators need a reliable supply of corn kernels, oil, sugar, and other ingredients. Delays in replenishment can interrupt an otherwise productive line.
Flavor changes and cleaning: Switching between caramel, cheese, chocolate, and other popcorn varieties may require cleaning and adjustments. The time required depends on the recipe, equipment design, and production procedures.
Coating and cooling limitations: Popped popcorn may need to wait if the coating drum, cooling conveyor, or seasoning equipment cannot keep pace with the popping stage.
Packaging speed: Finished popcorn can accumulate before the packaging station if bag filling, weighing, sealing, or packing operates more slowly than upstream equipment.
Product quality losses: Unpopped kernels, burnt popcorn, inconsistent coating, and damaged products can reduce saleable output even when the machine continues running.
These factors should be recorded separately wherever possible. Otherwise, a factory may see lower output without knowing whether the main issue is the popping process, material supply, downstream equipment, or product quality.
How Does Production Line Design Affect Efficiency?
In industrial popcorn manufacturing, production efficiency depends on how well the different processing stages work together. A fast popping machine cannot deliver its full potential if cooling, coating, conveying, or packaging becomes a bottleneck.
The following image illustrates the main equipment in an industrial popcorn production and coating line, including the popping system, ingredient feeding components, coating equipment, and conveyors.
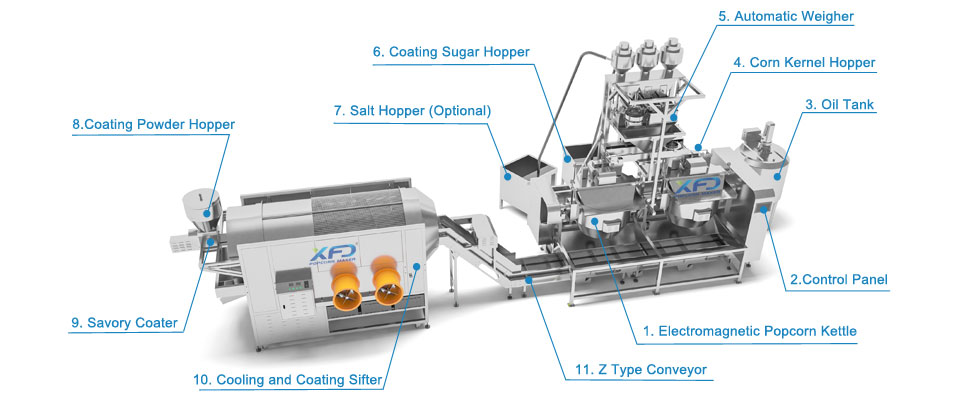
An integrated production system can coordinate several operations, including:
- Popping kernels using the selected heating technology.
- Supplying oil and other ingredients at the required rate.
- Transferring popcorn between processing stages.
- Applying seasoning, caramel, or other coatings.
- Cooling and filtering popcorn before the next stage.
- Preparing finished popcorn for weighing and packaging.
XFD's published automated batch popcorn production line uses electromagnetic heating and includes equipment for oil feeding, conveying, cooling, and coating. XFD lists a capacity of approximately 60–80 kg/h for this particular configuration.
This specification is a useful reference for equipment selection, but it should not be treated as a guarantee of actual factory output. Final production depends on the selected configuration, recipe, operating conditions, and the capacity of the complete processing system.
Factories with higher output requirements can also compare hot-air production systems, which may be configured with multiple poppers and caramelizers to meet larger production targets.
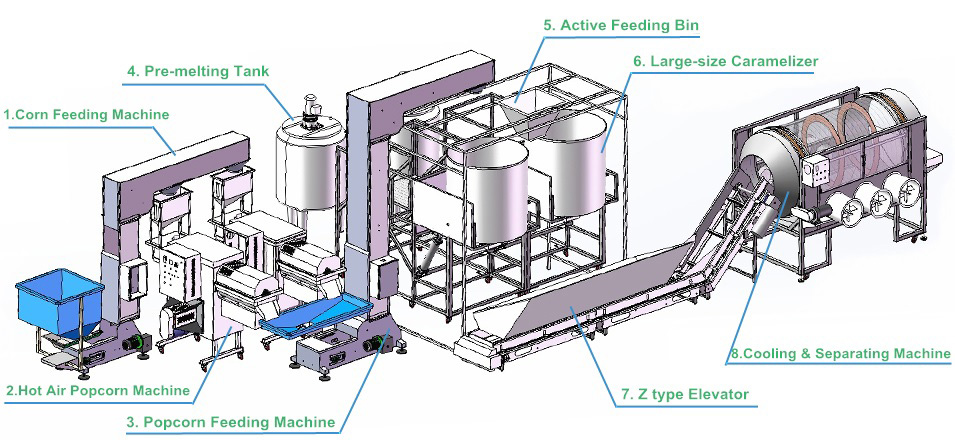
For factories evaluating a hot-air system, XFD's industrial hot-air popper and caramelizer production line is one option to review. Buyers should confirm the actual output of the proposed configuration and ensure that the coating and cooling stages can keep up with the popping equipment.
How Can Automation Improve Actual Output?
Automation can improve production efficiency by reducing repetitive manual work, coordinating equipment operations, and helping maintain a more consistent production flow. However, the actual improvement depends on the production process and the factory's existing limitations.
For example, automatic oil feeding can reduce interruptions associated with manual replenishment. Automated kettle discharge can help standardize batch transfer, while conveyors can reduce manual handling between production stages.
Automatic temperature controls and production monitoring can also help operators identify abnormal conditions earlier. When combined with appropriate cleaning and maintenance procedures, these features can support more consistent operation.
The following image shows XFD's fully automatic electromagnetic popcorn production and coating line. The integrated equipment layout illustrates how multiple processing stages can be brought together in a single production system.
Nevertheless, automation does not eliminate every production loss. Ingredient shortages, flavor changes, packaging delays, and equipment maintenance still affect actual output. A factory should evaluate the expected improvement against its current production records rather than assuming that a fully automatic line will always operate at its rated capacity.
Before purchasing equipment, buyers should confirm which processes are automated, which tasks still require operators, and whether the quoted production rate applies to the complete line or only to a specific machine.
How Should Factories Measure Production Efficiency Every Shift?
A consistent production report makes it easier to compare shifts, identify recurring losses, and evaluate whether equipment changes are delivering measurable results.
At a minimum, factories should record the following information:
- Rated capacity: The manufacturer's specified output for the selected equipment and product conditions.
- Scheduled production time: The total shift time allocated to production.
- Actual running time: The time the line was operating and producing.
- Finished output: The total quantity of completed popcorn produced during the measurement period.
- Saleable output: The quantity that meets product quality requirements and can be sold.
- Downtime: The duration and reason for each significant interruption.
- Product changeovers: The time required to switch recipes, flavors, or packaging formats.
- Material consumption: The amount of kernels, oil, coating ingredients, and packaging materials used.
It is useful to distinguish actual production from saleable production. A line may produce 600 kg of popcorn during a shift, but if 20 kg fails inspection, the saleable output is only 580 kg.
Factories can also calculate effective hourly output using the following formula:
Effective Hourly Output = Total Finished Output ÷ Scheduled Production Time
If a factory produces 580 kg of saleable popcorn during an eight-hour scheduled shift, its saleable output rate is 72.5 kg/h. This figure includes the effect of downtime and other interruptions that occur within the scheduled period.
For meaningful comparisons, factories should use the same measurement rules from shift to shift. They should also separate planned breaks and scheduled maintenance from unplanned downtime when analyzing the reasons for lost production time.
When Should a Popcorn Factory Upgrade Its Production Line?
A factory should consider an upgrade when its existing equipment repeatedly fails to meet demand, when production bottlenecks limit finished output, or when labor and operating costs become difficult to manage.
However, buying a higher-capacity machine is not always the first or best solution. Before making an investment, managers should review production records and determine whether the main constraint is insufficient popping capacity, slow coating, limited cooling capacity, packaging speed, or avoidable downtime.
For example, a factory targeting 100 kg of finished popcorn per hour may not achieve that target with a production line rated at 80 kg/h. Even under ideal conditions, the rated capacity is below the required output. A higher-capacity configuration may be necessary, subject to confirmation of the actual finished-product rate.
By contrast, if the popping equipment already has sufficient capacity but the packaging station causes frequent queues, improving the packaging process may deliver better results than replacing the entire popping system.
When evaluating a new industrial popcorn production line, factories should provide the supplier with their target output, popcorn varieties, operating hours, packaging requirements, and expected future demand.
What Should Buyers Confirm Before Purchasing Popcorn Equipment?
Rated capacity is an important starting point, but it should not be the only specification used to compare industrial popcorn machines. Buyers need to understand how the equipment will perform within their intended manufacturing process.
Before confirming an order, ask the supplier the following questions:
- Does the rated capacity refer to raw kernels, popped popcorn, coated popcorn, or finished packaged product?
- Under what recipe and operating conditions was the stated output measured?
- How much setup, cleaning, and changeover time should be expected?
- Can the cooling, coating, conveying, and packaging equipment handle the same production rate?
- What staffing, electrical supply, floor space, and maintenance access are required?
- Can the production line be expanded if demand increases?
- Can the supplier demonstrate the equipment using the intended recipe and define an agreed method for measuring output?
These questions help buyers compare equipment on a consistent basis and avoid choosing a machine solely because it has a higher advertised capacity.
XFD specializes in popcorn equipment, from individual machines to integrated industrial production solutions. Factories can discuss their production targets and review available equipment through the XFD popcorn equipment website.
Frequently Asked Questions About Popcorn Production Efficiency
What is the difference between rated capacity and actual output?
Rated capacity is the specified production rate under defined conditions, while actual output is the quantity produced during a real operating period. Actual output is affected by downtime, cleaning, product changeovers, equipment coordination, and quality losses.
How do you calculate popcorn production efficiency?
Divide actual output by rated output for the same period and multiply by 100%. For example, if a line produces 520 kg during an eight-hour shift against a rated capacity of 80 kg/h, its rated output is 640 kg and its output-based production efficiency is 81.25%.
Can an industrial popcorn machine maintain its rated capacity throughout an entire shift?
Not necessarily. Rated capacity depends on specified operating conditions. Cleaning, maintenance, ingredient replenishment, flavor changes, and downstream bottlenecks can reduce the actual output achieved during a full shift.
What is the capacity of XFD's industrial popcorn production line?
XFD offers industrial popcorn production configurations with different capacity specifications. For example, its large-scale electromagnetic popcorn production and coating line is listed at approximately 60–80 kg/h, while its fully automatic electromagnetic production line is listed at 120–160 kg/h. Buyers should confirm the selected configuration and the expected finished-product output for their recipe and operating conditions.
How can a popcorn factory increase actual production output?
Start by recording output and downtime, then identify the main bottleneck. Improvements may include reducing changeover time, stabilizing ingredient supply, coordinating popping and coating equipment, improving cooling and packaging flow, or upgrading the specific equipment that limits production.
Does a higher rated capacity always mean better production efficiency?
No. A higher rated capacity does not guarantee a higher percentage of production efficiency or lower operating costs. The best equipment is the configuration that meets the factory's actual demand while maintaining product quality, reliable operation, and a balanced production flow.
Why should factories measure saleable output separately from total output?
Total output includes all product produced, while saleable output excludes popcorn that fails quality requirements. Measuring both helps factories understand whether production losses come from equipment performance or product defects.
What should buyers check when comparing popcorn production line suppliers?
Confirm the capacity measurement basis, operating conditions, automation scope, downstream equipment capacity, maintenance requirements, and the method used to verify output. Where possible, request a production test using the intended recipe and agree on how finished output will be measured.