In wet flue gas desulfurization (WFGD) systems, the limestone grinding circuit is often regarded as a supporting function—indispensable, yet hardly strategic. This view is not correct. The grinding process directly determines the reactivity of the desulfurization reagent, the operational reliability of the system, and a considerable portion of the plant's auxiliary power consumption. For plants pursuing lower operating costs and higher SO₂ removal efficiency, the choice of mill technology is one of the most far-reaching decisions in FGD design.
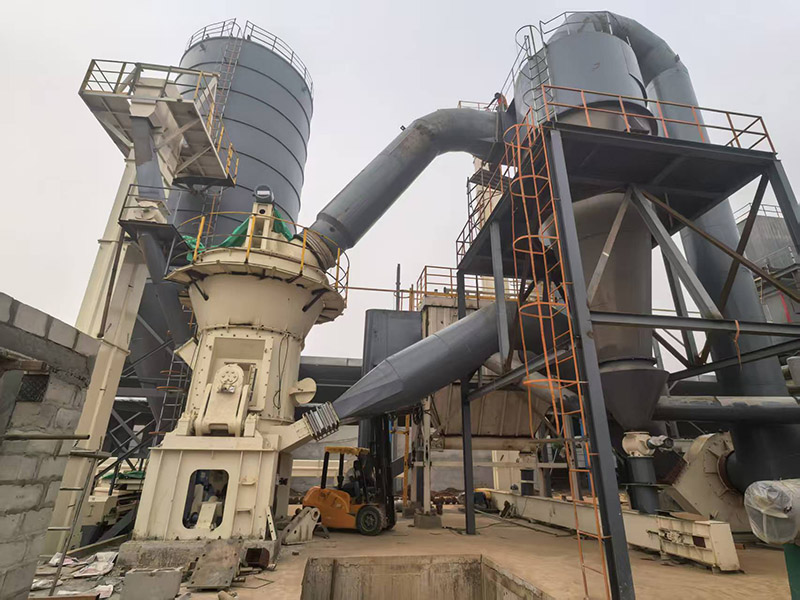
Drawing on comparative studies from operating power stations and pilot-scale test data, this article demonstrates—from both technical and economic perspectives—why the vertical roller mill (VRM) is the superior grinding solution for limestone preparation in wet FGD applications.
Understanding the Role of Limestone Grinding in FGD
The wet limestone-gypsum process remains the dominant FGD technology globally, valued for its high desulfurization performance and the widespread availability of limestone as a reagent . In this process, finely ground limestone (CaCO₃) is slurried with water and sprayed into an absorber tower, where it reacts with SO₂ in the flue gas to form calcium sulfite, which is subsequently oxidized to produce saleable gypsum (CaSO₄·2H₂O) .
The dissolution rate of limestone is a critical kinetic constraint. Limestone has low solubility—approximately 50 mg/L—which means the surface area available for reaction directly limits SO₂ removal efficiency . To compensate, limestone is typically ground to a fineness of 90–95% passing 45 μm (325 mesh) before entering the absorber . Achieving this particle size distribution consistently and efficiently is the primary function of the grinding circuit.
A poorly performing grinding circuit manifests in several ways: increased limestone consumption due to incomplete reagent utilization, reduced gypsum purity, higher solid waste volumes, and diminished system reliability . Conversely, over-grinding wastes energy without proportional process benefits. The optimal grinding solution must deliver precise fineness control with minimal energy input and maximum availability.
The Conventional Route: Wet Ball Milling
For a long time, the mainstream configuration for limestone preparation has been the wet, closed-circuit ball mill. In this system, limestone and water are fed into the mill in proportion, and the resulting slurry is classified by cyclones. Coarse particles are returned to the mill for further grinding, while the cyclone overflow—at a solids concentration of about 30%—is sent to the absorber as the desulfurization reagent.
Ball mills are robust in construction and mature in process, which explains their long-standing dominance in the industry. But when used for limestone slurrying, their inherent shortcomings are equally evident. A substantial portion of this energy is not used for particle size reduction, but is wasted as heat and noise. At the same time, ball mills occupy a large footprint, and the grinding media and liners are subject to continuous wear, driving up consumable costs.
More notably, ball mills struggle to meet the fineness requirements of modern FGD systems. When the product specification is raised to 95% passing 45 μm, the increase in energy consumption for ball milling becomes disproportionately large.
How the Vertical Roller Mill Works?
The motor drives the grinding disc to rotate through the reducer. Material falls from the feed inlet onto the center of the grinding disc, while hot air enters the mill from the air inlet. Under the action of centrifugal force, the material moves toward the edge of the grinding disc. As it passes through the annular groove on the grinding disc, it is crushed under the pressure of the grinding rollers. The crushed material is lifted by the high-speed airflow at the edge of the grinding disc, while larger particles fall back onto the grinding disc to be re-ground. When the material in the airflow passes through the dynamic powder classifier, under the action of the rotating rotor, coarse powder falls back onto the grinding disc to be ground again. Qualified fine powder is carried out by the airflow and collected in the dust collector, becoming the final product. Material containing moisture is dried through contact with the hot gas, achieving the required product moisture.
Product Main Features:
1. High efficiency and energy saving: High grinding efficiency, with energy consumption 40% lower than that of ball mills;
2. Low overall investment cost: Simple process flow and small footprint, only 50% of that of a ball mill;
3. High reliability: The entire machine adopts a modular component design, with highly mature components;
4. Convenient maintenance and low operating cost: Low wear, convenient inspection and repair operations, and a high degree of automation;
5. Stable product quality: Short material residence time, easy to distribute and detect, and stable product quality;
6. Environmentally friendly and low-carbon: Low system vibration, low noise, fully sealed, with no dust leakage.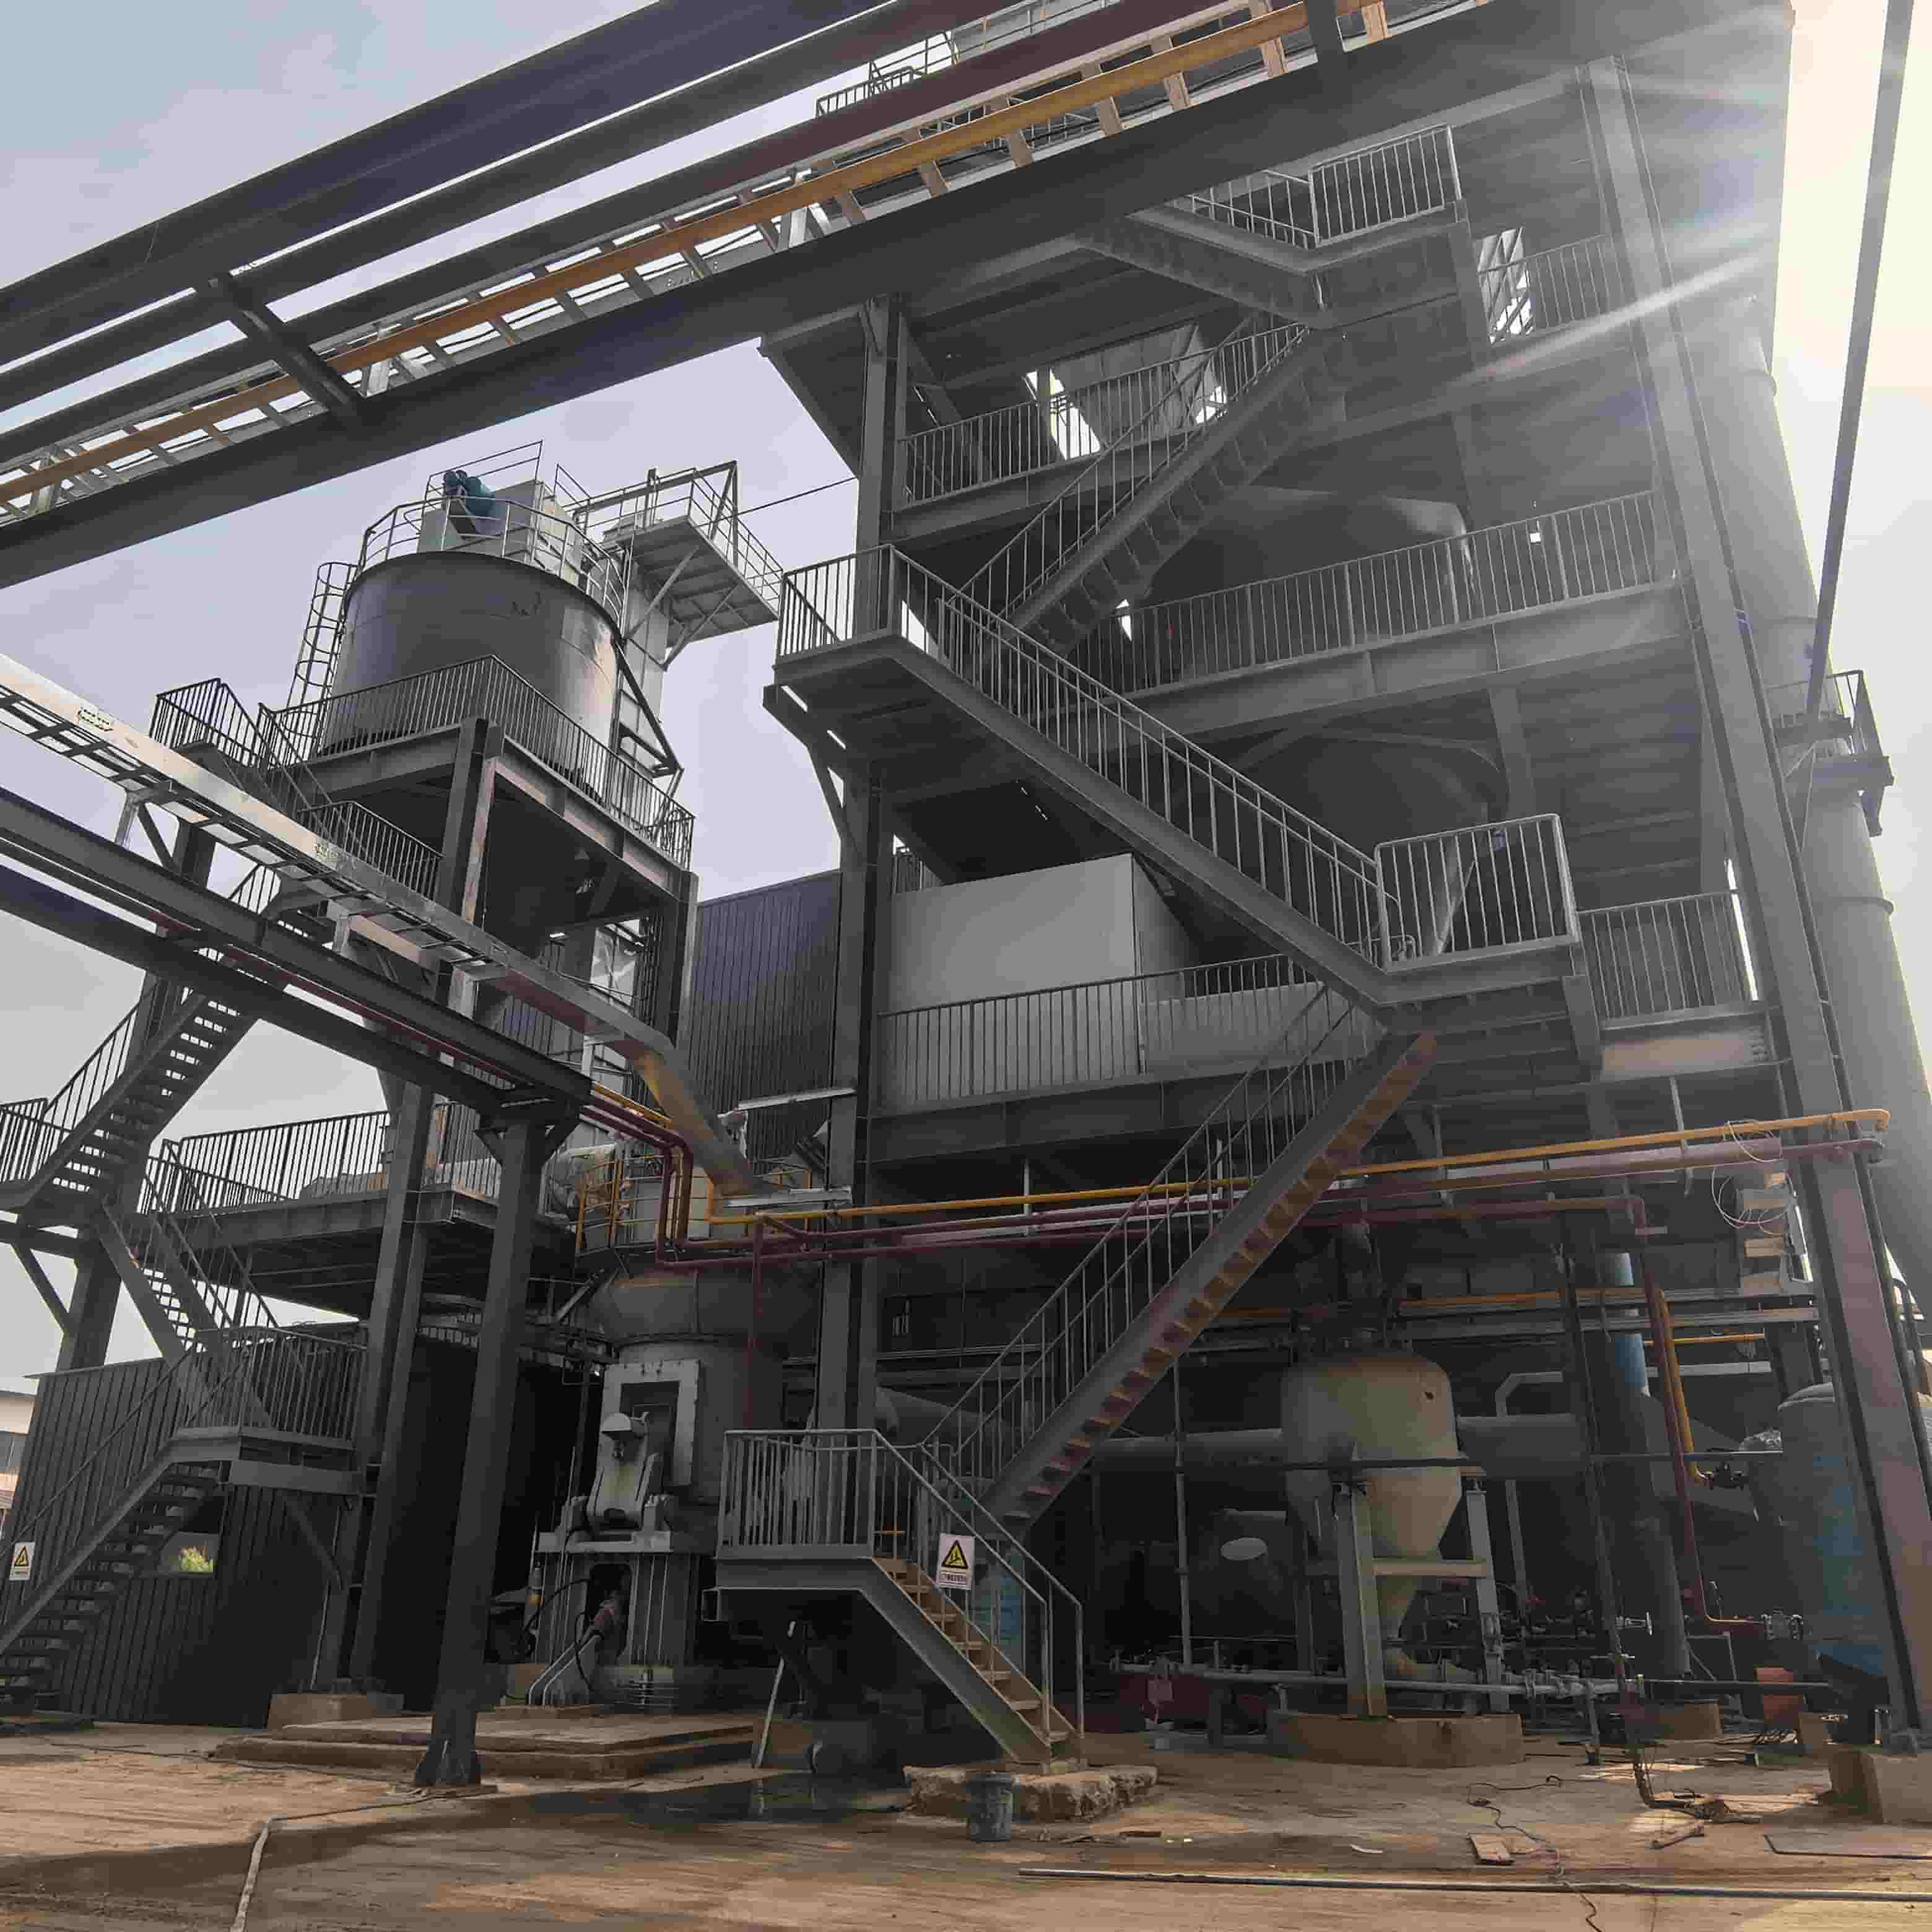
Conclusion
Choosing a limestone grinding system for flue gas desulfurization is not merely a procurement decision—it is a long-term commitment to a specific operating cost structure and maintenance regime. The evidence from comparative technical and economic studies is clear: compared with conventional wet ball milling, the vertical roller mill offers significantly lower energy consumption, reduced wear part costs, more precise product control, and higher financial returns.
For power plants designing a new flue gas desulfurization system or considering an upgrade to an existing limestone preparation circuit, the VRM represents a proven and economically compelling alternative to the ball mill paradigm. As emission regulations tighten and auxiliary power consumption comes under increasing scrutiny, the case for adopting the VRM will only grow stronger.
FAQ
Q1: What is limestone grinding in FGD, and why is it necessary?
A: Limestone grinding reduces limestone to a fine powder (typically 90–95% passing 45 μm) so it can react efficiently with SO₂ in the absorber. Without fine grinding, reagent utilization drops and gypsum purity suffers.
Q2: Why is a vertical roller mill (VRM) preferred over a ball mill for FGD limestone grinding?
A: The VRM uses significantly less energy, eliminates grinding media costs, and offers more precise fineness control in a smaller footprint. Although its upfront cost is higher, it delivers better NPV and a shorter payback period.
Q3:What fineness should limestone be ground to for wet FGD?
A: Most wet FGD systems specify 90–95% passing 45 μm (325 mesh). This balances reagent reactivity against grinding energy.
Q4:Can limestone be milled off-site using VRM technology?
A: Yes, because the VRM produces a dry powder, grinding can take place at the limestone mine and the product transported to site. This can cut mechanical equipment costs by over 90% compared to an on-site wet ball mill circuit.
Q5:Does a VRM require drying, and how is that handled?
A: A VRM performs grinding, drying, and classification in a single unit. Hot gas is introduced into the mill to evaporate feed moisture during grinding, eliminating the need for separate drying equipment.
Q6:What maintenance does a VRM require in limestone service?
A: Maintenance focuses on the grinding rollers and table liners, which use wear-resistant materials. Bed grinding causes less wear than ball milling, and consumables dropped from 2.8% of OPEX to just 0.5% in the Kusile study.
Q7:How much space does a VRM system save compared to a ball mill circuit?
A: A VRM integrates grinding, drying, and classification in one vertical unit, reducing floor space by up to 50%. This is especially valuable for retrofits with limited space.
Q8:Is VRM technology proven in FGD applications?
A: Yes, VRMs have been used in cement and mineral processing for decades and are well established in FGD limestone grinding. Comparative studies at operating power stations have validated their performance and financial returns.